Assembly Capabilities
Put It All Together, Under One Roof
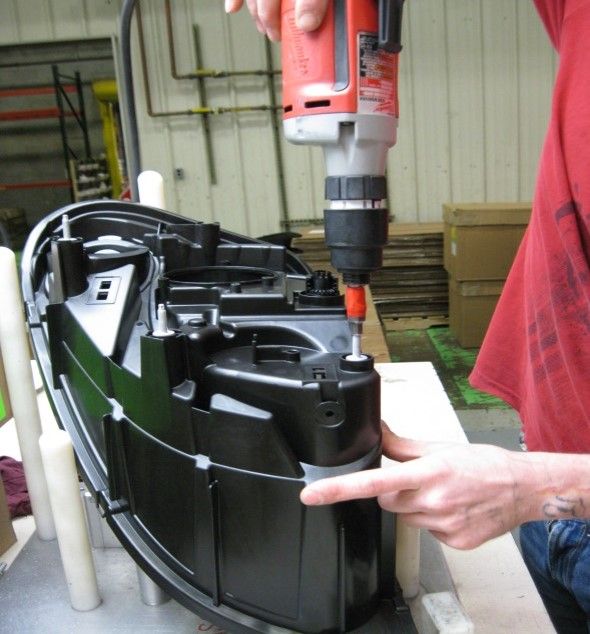
Put it all together. As your full-service plastics manufacturer, we can decorate, assemble, and package your products to cut lead times, reduce costs, shorten the supply chain, and maintain quality throughout the production process. We can customize fully automated processes for your particular assembly, assemble it manually, or perform a hybrid of the two.
Some of the value-added assembly operations we offer include:
- Insert Molding
- Over molding
- EMI/RF shielding
- Insert heat staking
- Sonic welding
- Part decorating
- Pad printing
- Hot stamping
- Post-molding plastic painting
- Post-molding chrome plating
- Precision hand-manual assembly
- No defect leak detection
- Precision hole taping
- Custom packaging and kitting
Request a Free Consultation
Learn With EnTech
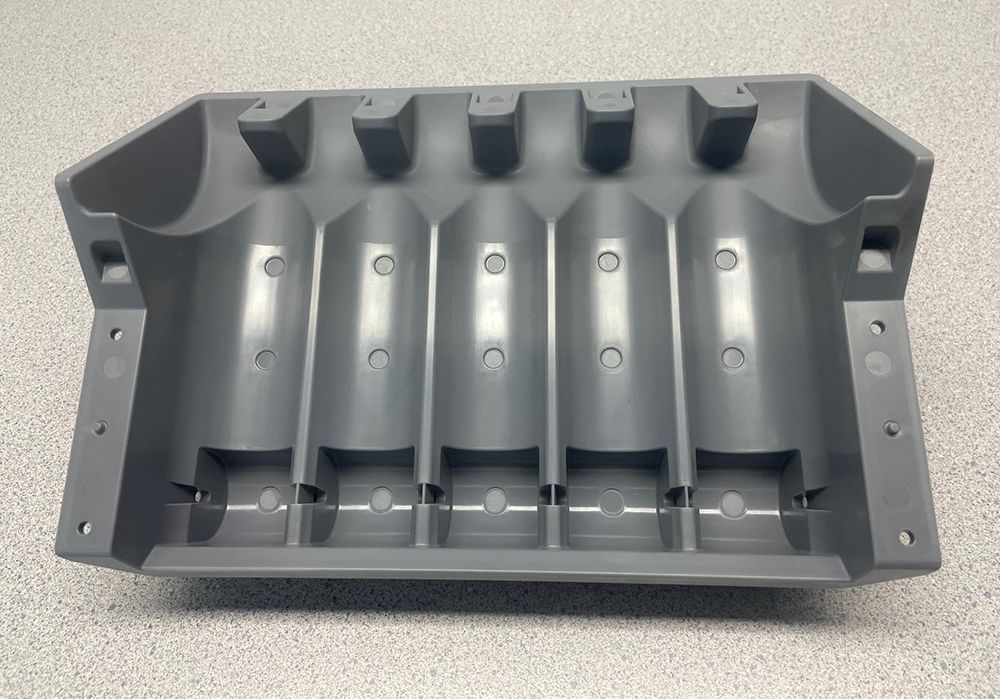
When a component needs to operate in a high temperature environment, resin selection becomes a complex conversation. Getting it wrong can lead to component softening, mechanical failure and even equipment contamination. At EnTech Plastics, we carefully analyze the environments in which components must perform and we pay attention to all the details. What industrial machines run at a high temperature requiring specific resins? Ovens, dryers, motor assemblies, lighting fixtures and heat-adjacent industrial equipment all make the list. In this blog, we will take a look at how PEI, PPS, PEEK and other high-heat materials behave once tooling, molding conditions and long-term aging enter the picture. What should I know about maximum service temperature? Maximum service temperature is the highest limit of heat a material can handle safely for a long period of time. While resin datasheets showcase this number, that continuous use temperature describes a resin sitting in isolation under controlled conditions. It is not taking into account a molded, geometrically complex part carrying mechanical load, chemical exposure and thermal cycling all at once. Sustained mechanical stress or exposure to cleaning chemicals can contribute to a material fatiguing faster than with just steady-state heat. When engineers design around the full operating conditions the maximum service temperature is much more accurate and reliable. What is heat deflection temperature (HDT)? HDT measures the temperature at which a material begins to deform under a specified load. It is typically tested at 0.45 MPa or 1.82 MPa. This number gives a much clearer picture of real-world performance than continuous use temperature alone. It includes stiffness retention under load, not just chemical stability. This number matters most for components like motor housings, structural brackets near heat sources or any part that has to hold a tight tolerance or maintain a seal while hot. A resin can be thermally stable, meaning it doesn’t degrade or off-gas, while still going soft enough under load to warp, sag or lose critical fit. For parts that need to maintain dimensional integrity while under clamping force, spring load or its own weight at elevated temperature, HDT at the higher load value (1.82 MPa) is ideal. What is thermal expansion and why does it cause machine failures? When a part fails, coefficient of linear thermal expansion (CLTE), is often the root cause. Every plastic expands and contracts more than metal as temperature changes and when a molded component is mated to metal fasteners, inserts, or housings, mismatched expansion rates create stress at every thermal cycle. The result is loosened fasteners, cracked bosses around metal inserts, warped mounting flanges or seals that leak once the assembly cools back down from operating temperature. Designing for thermal expansion means thinking not just about the resin’s absolute temperature ceiling, but about how it will move relative to everything it’s fastened, bonded or press-fit against across the full expected temperature range. How does long-term thermal aging affect a machine? A resin’s initial mechanical properties are not indicative of what it will look like after years of sustained heat exposure. Long-term thermal aging describes how tensile strength, impact resistance and dielectric properties degrade over extended exposure at a given temperature. Some materials maintain their mechanical properties after thousands of hours at elevated temperature, while others degrade steadily, becoming brittle or lose impact strength well before they reach any dramatic failure point. If you need a machine to run for more than 10 years, think about industrial ovens, dryer components, motor assemblies, etc., thermal aging data is a vital piece to material selection. What are the differences in PEI, PPS, PEEK and other high-heat resins? Polyetherimide (PEI) PEI is a great choice for lighting components, electrical connectors and structural brackets near heat sources. Its natural transparency (in unfilled grades) is a differentiator for lighting and sight-glass applications. High heat deflection temperature Inherent flame resistance Dimensional stability Amorphous resin Because it’s amorphous rather than semi-crystalline, PEI doesn’t experience the same shrinkage variability tied to cooling rate that crystalline resins do. Polyphenylene Sulfide (PPS) PPS is ideal for motor components, pump housings and other parts exposed to oils, fuels or aggressive cleaning chemicals alongside sustained heat. PPS (glass-filled grades) is common in automotive and industrial motor applications where heat, chemical exposure and dimensional stability all matter at once. Semi-crystalline resin Solid chemical resistance Inherent flame retardance Strong dimensional stability Because PPS is semi-crystalline, its final mechanical and thermal performance is more sensitive to processing conditions than PEI’s. PEEK (Polyether Ether Ketone) PEEK is ideal for industrial machinery applications. Outstanding continuous use temperature Exceptional mechanical strength retention at elevated temperatures Excellent chemical and wear resistance Strong long-term thermal aging performance. PEEK earns its premium price tag in applications where failure isn’t an option. The right question isn’t whether PEEK can handle your application, it’s whether your application actually needs it. High-Heat Contenders Depending on the application, materials like polyamide-imide (PAI), liquid crystal polymer (LCP), and high-heat polyamides (such as PA6T or PA9T) are also on the list. LCP offers extremely low CLTE and excellent dimensional stability in thin-wall parts, making it a candidate for connectors and precision components near heat sources where PPS or PEI might not hold tolerance as tightly. Why does the molding process change the thermal performance? The same resin, molded two different ways, can deliver meaningfully different thermal performance in the finished part. This is especially true for semi-crystalline materials like PPS, where mold temperature and cooling rate directly influence the degree of crystallinity achieved. Higher crystallinity generally improves heat deflection temperature, chemical resistance, and dimensional stability. This requires molding at a higher mold temperature and longer cooling rates that a molder chasing fast cycle times might not be inclined to use. Achieving the crystallinity a demanding thermal application actually requires means controlling mold surface temperature, packing pressure and cooling time deliberately. Making the Resin Choice Specifying a high-temperature resin is a set of interconnected tradeoffs between continuous use temperature, HDT under realistic load, thermal expansion relative to mating components, long-term aging behavior, and how the molding process itself will influence the properties you actually get in a finished part. At EnTech, we work with engineers before a tool is ever cut. Whether you’re designing a component for a dryer interior, a motor assembly, a lighting fixture, or any other heat-adjacent industrial application, getting the resin selection and molding process right the first time saves you the far more expensive lesson of a field failure discovered after the part is already in service. Working through a high-temperature application? Talk to our engineering team about resin selection, tooling considerations and process controls for your next demanding project.
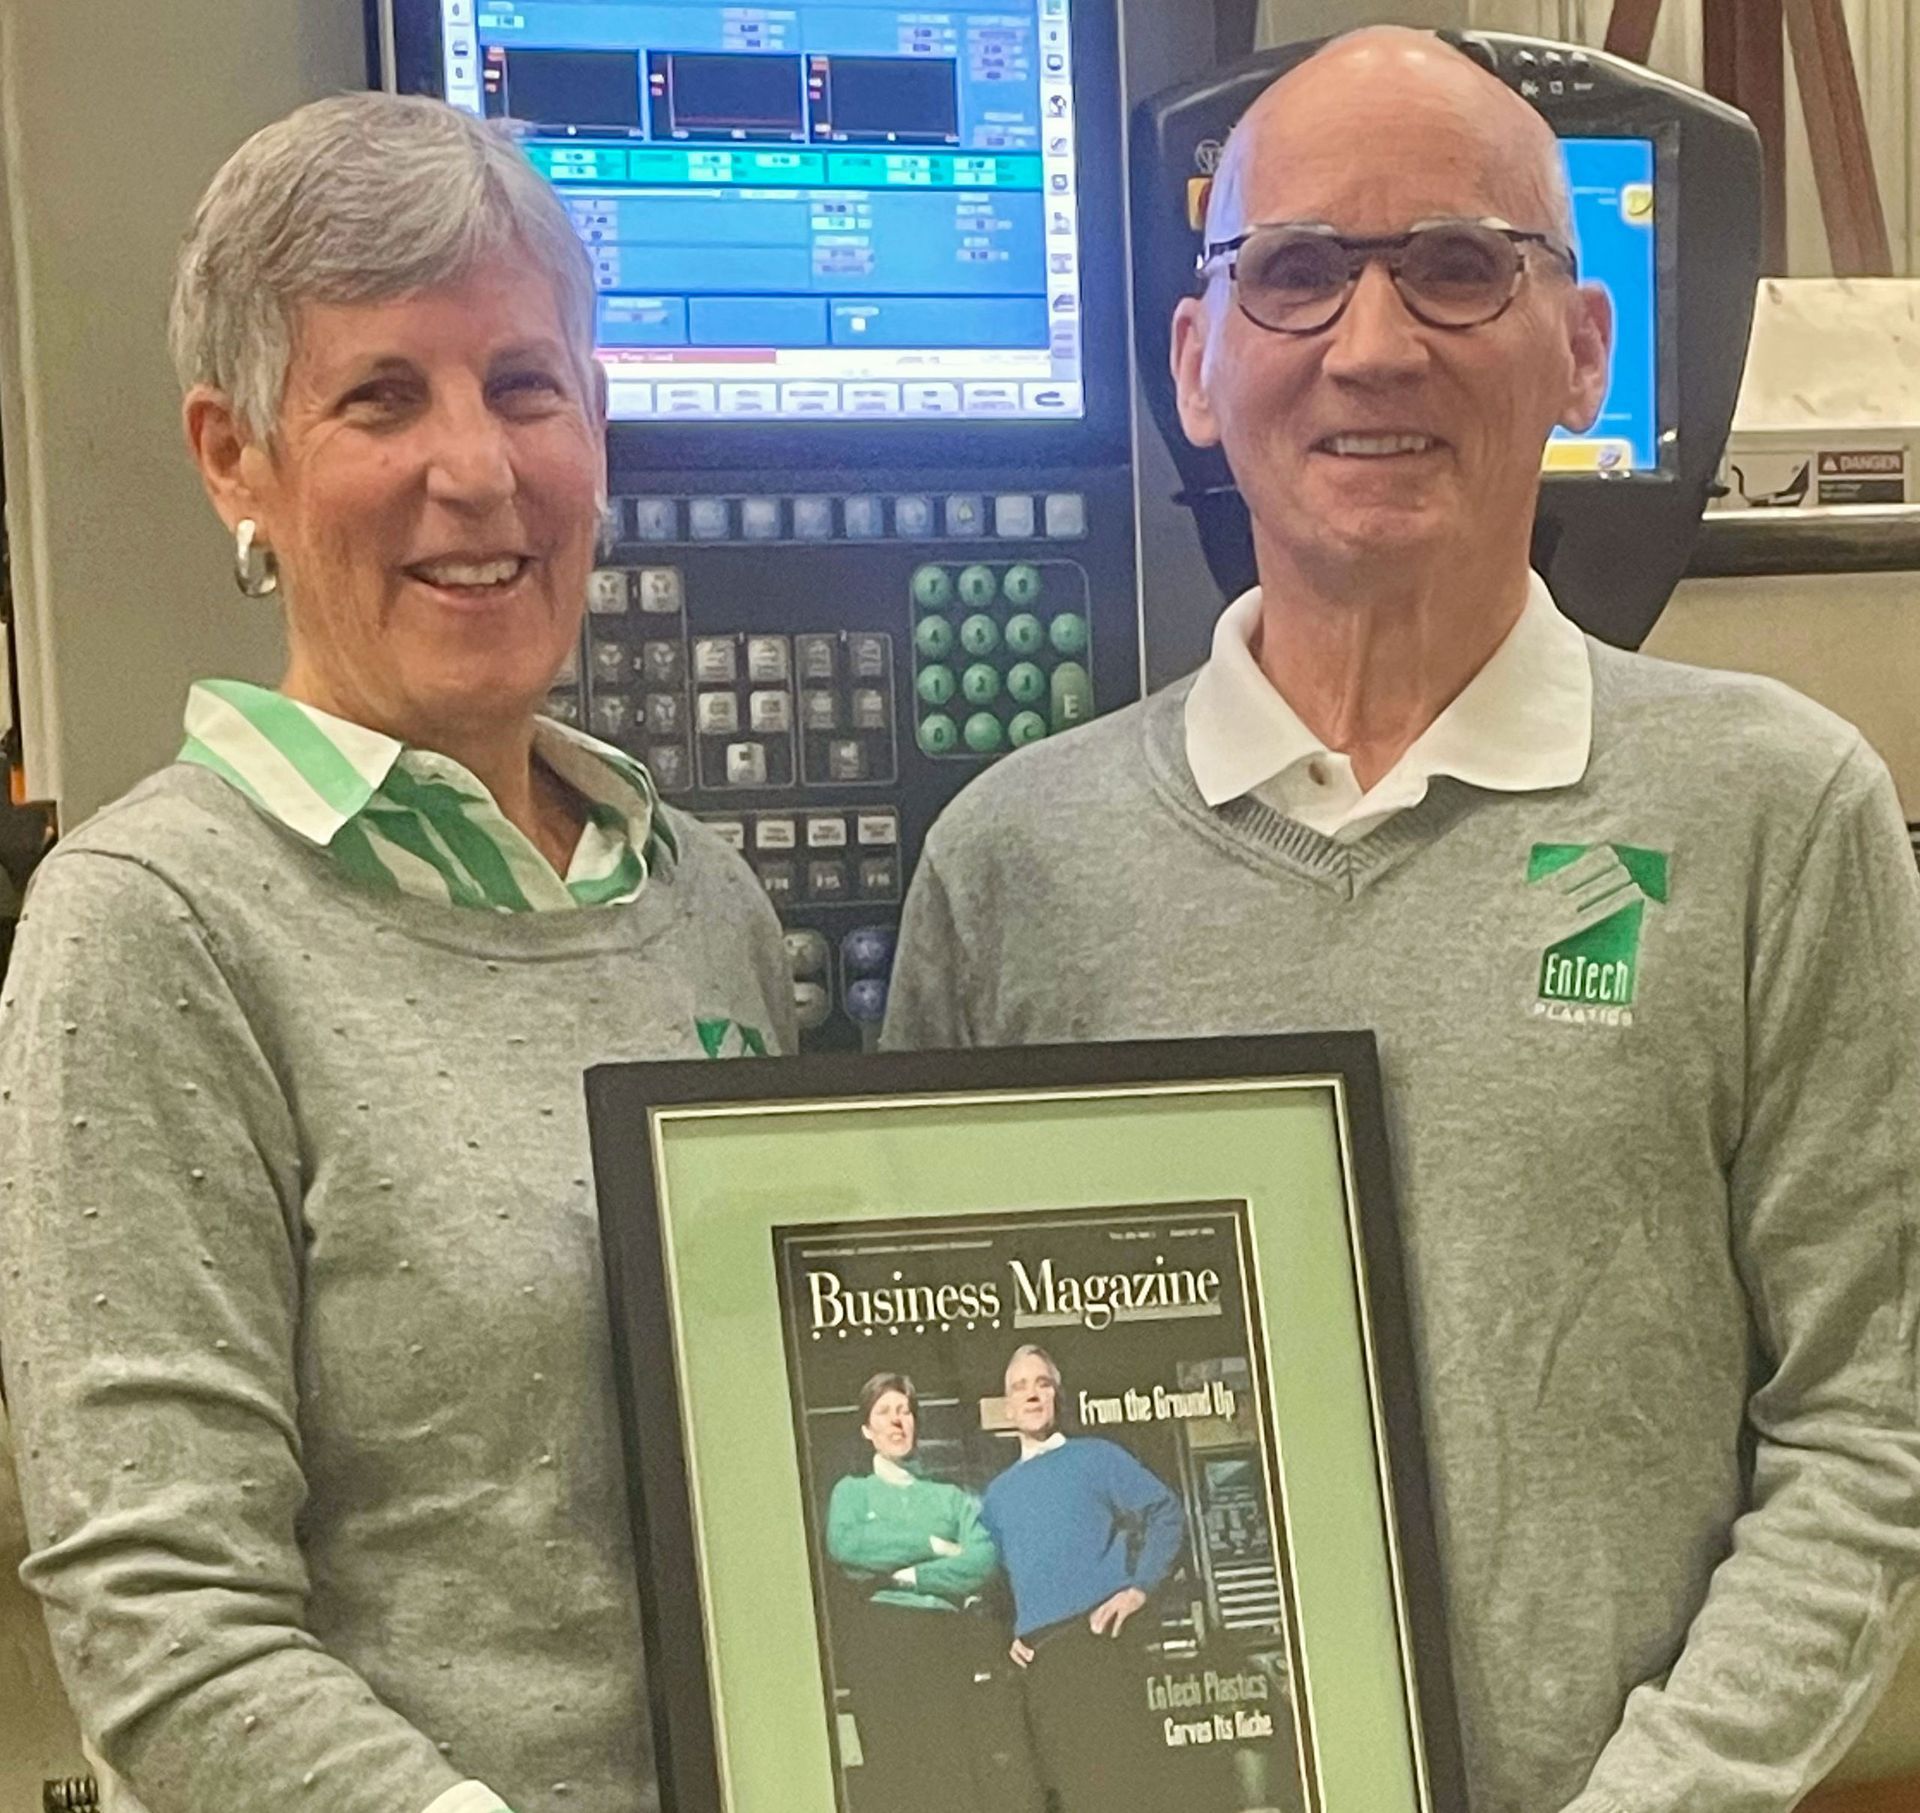
Although EnTech Plastics is celebrating its 30th anniversary this year, the seeds for the business were planted over 45 years ago. When Kevin Gearity was in high school, he spent summers working in a small costume jewelry manufacturing plant. There he discovered his fascination with manufacturing and all the challenges associated with running a manufacturing operation. Having decided on a career in manufacturing and seeing the potential offered by a degree in engineering, Kevn graduated from Stevens Institute of Technology in Hoboken, NJ, with a bachelor’s degree in mechanical engineering. He later followed that up at Carnegie Mellon with a Masters degree in Industrial Administration, majoring in Operations Management. After graduating, Kevin gained great experience working for Fortune 100 Companies including IBM and Johnson & Johnson. Though that experience was invaluable, Kevin felt something was missing. He realized that he could have a bigger impact by working at smaller companies so he decided to pursue opportunities at smaller manufacturing companies in the metalworking and plastics industries. After joining a plastics manufacturing company, Kevin furthered his engineering education by obtaining 33 credits in Plastics Engineering courses at Penn State University. While working for smaller, family-owned businesses, Kevin realized that he was the type of individual who had what it takes to run his own business. Despite the risk and with three young kids at home, Kevin founded EnTech Plastics and began operations with two injection molding machines in 1996.
At EnTech Plastics, we treat wear resistance as an engineering problem and we consider tribology when specifying resins for custom injection molding.